Choosing the right Industrial Aluminum Profile in 2026 requires more than comparing prices and wall thicknesses. The decision affects frame rigidity, assembly time, maintenance, and long-term energy use. A profile that looks strong in a catalog may twist under vibration or fail around poorly designed joints.
Industry data shows why this choice matters. The International Aluminium Institute reported global primary aluminium production of about 70.6 million metric tons in 2023. Demand continues across automation, construction, logistics, and renewable-energy equipment. Grand View Research also identifies aluminum extrusion as a growing market, supported by lightweight designs and modular manufacturing. These figures provide direction, not a final specification. Actual performance depends on alloy, temper, cross-sectional geometry, surface treatment, and load conditions.
Details matter.
This guide explains how to evaluate profiles for real industrial environments. It considers 6063-T5 and 6061-T6 alloys, allowable deflection, slot compatibility, fastener access, and corrosion exposure. It also examines supplier evidence, including mill certificates, dimensional tolerances, testing records, and quality systems such as ISO 9001. European Aluminium’s circularity reports further emphasize recycled content and design for material recovery. However, recycled content alone does not prove suitability. A higher-strength profile is not always the better choice. It may cost more, weigh more, or complicate machining. Even experienced buyers can overlook joint stiffness and installation errors. Careful selection should connect the published data with the actual load, environment, assembly method, and service life expected in 2026.
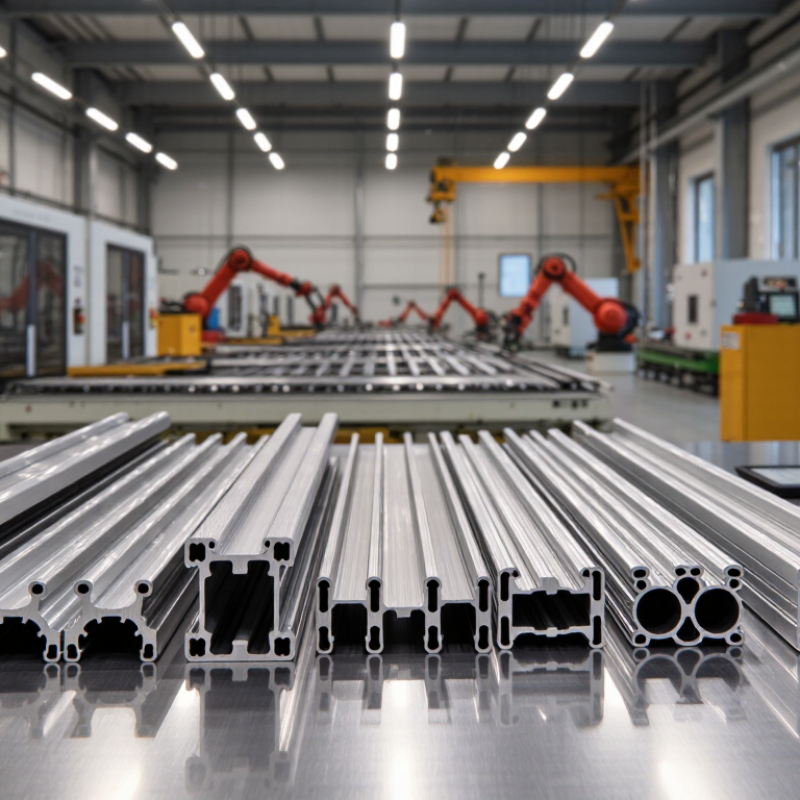
Start with the load. Record the total weight, force direction, and whether the load stays still or moves repeatedly. A conveyor frame carrying 80 kilograms behaves differently from a guard panel with occasional contact. Include cables, tools, vibration, and unexpected impact. Small omissions can create large deflection.
Measure the unsupported span between mounting points. Longer spans usually need deeper profiles or closer supports. Set a practical deflection limit before comparing profile sizes. For precision equipment, even a few millimeters may affect alignment. For a protective frame, that movement may be acceptable. Calculate bending stress and deflection with an engineer when safety or accuracy matters. My first estimate is not always reliable, especially when loads are off-center.
Tolerance is not decoration. Check profile dimensions, straightness, twist, slot position, and cut-length accuracy. Connecting plates and linear components may require tighter machining than the extrusion itself. Do not assume every profile fits interchangeable hardware. Review current technical data and confirm measurements with sample parts.
Tips: Build a simple load table. Mark each support location. Separate static and moving loads. Specify allowable deflection in millimeters. Ask for inspection records when tolerances are critical. Leave adjustment slots where alignment may change. Test one assembled section before ordering the full structure. A perfect calculation can still miss real-world vibration.
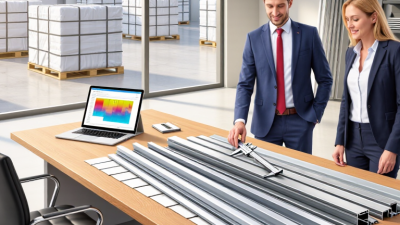
When choosing an industrial aluminum profile, density rarely separates 6063-T5 from 6061-T6. Both are commonly estimated at 2.70 g/cm³, so weight depends mainly on profile geometry and wall thickness. The meaningful difference is mechanical performance. 6061-T6 usually provides higher tensile and yield strength. It suits brackets, machine frames, supports, and parts exposed to repeated loading. However, strength alone does not guarantee a safe design.
6063-T5 is widely selected for profiles requiring smooth extrusion, clean surfaces, and consistent appearance. It works well for guards, rails, covers, light frames, and architectural sections. Its strength is lower than 6061-T6, so engineers should avoid using it for heavily loaded joints without calculation. In workshop checks, sharp corners and thin walls often cause more trouble than the alloy choice. Small details matter.
Review the expected load, span, connection method, and operating temperature. Then verify the supplier’s temper and inspection documents. Published values can vary with section size and manufacturing conditions. A profile may feel rigid by hand but still deflect under a long-term load. I have seen this mistake in prototype work. It looked acceptable at first. Bolts, slots, and local crushing later changed the result. Use 6063-T5 for efficient extrusion and finish. Choose 6061-T6 when higher strength justifies more demanding fabrication. Check the actual section before approval.
How to Choose Industrial Aluminum Profiles in 2026?
Select Section Geometry by EN 755-9 Dimensional Tolerance Classes
Start with function, not appearance. Under EN 755-9, profile geometry must match the required dimensional and form tolerances. Check wall thickness, width, height, corner radius, straightness, and twist against the relevant tolerance tables. A wide, thin flange may reduce weight, but it can increase distortion after extrusion. Deep ribs improve stiffness, yet they may require tighter control during assembly. Choose a tolerance class that supports the fit without creating unnecessary production costs.
Tolerance matters at the interface. For sliding covers, bearing seats, and bolted frames, small deviations can create visible gaps or difficult installation. For non-critical guards, standard tolerances may be adequate. Tighter tolerances should be specified only where measurements prove they are needed. Keep the drawing clear. Include the profile designation, alloy condition, critical dimensions, and inspection method. Do not assume every dimension needs the tightest class. That is a common mistake.
Tips: Mark critical surfaces directly on the drawing. Ask for sample measurements across several profile lengths. Review straightness after cutting, because processing can change the result. Check the current EN 755-9 edition before approval. One more thought: a perfect drawing cannot rescue a poorly supported profile during transport or machining.
| Profile Geometry | Typical Section Size (mm) |
Typical Wall Thickness (mm) |
Recommended EN 755-9 Tolerance Route | Dimensional Features to Control | Typical Industrial Use | Selection Consideration |
|---|---|---|---|---|---|---|
| Solid rectangular profile | 20 × 10 to 120 × 40 | Solid section | Standard tolerance | Overall width, overall height, corner radius, straightness and end squareness | Guide rails, support bars, brackets and machine frames | Use when the section is compact and load transfer is more important than internal weight reduction. |
| Solid round bar | 10 to 80 diameter | Solid section | Standard tolerance | Diameter, roundness, straightness and surface condition | Axles, spacers, shafts and machined components | Specify a tighter diameter requirement only when it is required for machining, bearing fits or sliding interfaces. |
| Hollow rectangular profile | 20 × 20 to 150 × 80 | 1.5 to 6.0 | Standard tolerance | Outside dimensions, wall thickness, corner radius, twist and straightness | Machine frames, guards, conveyor structures and enclosures | Choose a larger perimeter or thicker wall when stiffness and resistance to local denting are priorities. |
| Large hollow structural profile | 80 × 80 to 250 × 150 | 3.0 to 10.0 | Standard tolerance | Overall dimensions, wall thickness, flatness, twist and angular alignment | Heavy-duty frames, workstations and automated equipment bases | Confirm extrusion press capability and specify critical datum surfaces separately from non-functional surfaces. |
| Thin-wall hollow profile | 20 × 20 to 100 × 50 | 1.0 to 2.0 | Special tolerance by agreement | Wall thickness, local distortion, twist, corner radius and straightness | Lightweight covers, partitions and low-load assemblies | Thin walls are more sensitive to die design, cooling conditions and handling; avoid unnecessarily tight requirements. |
| L-angle profile | 20 × 20 × 2 to 100 × 100 × 10 | 2.0 to 10.0 | Standard tolerance | Leg lengths, included angle, leg straightness, corner radius and twist | Edge protection, mounting rails and structural bracing | Control the included angle when the profile mates with panels, plates or other extrusions. |
| T-section profile | 20 × 20 to 100 × 100 | 2.0 to 8.0 | Standard tolerance | Flange width, web height, flange thickness, angle and straightness | Stiffeners, mounting tracks and load-distribution members | Use the flange as the primary datum when the profile is assembled against a flat plate. |
| U-channel profile | 20 × 15 to 150 × 75 | 2.0 to 8.0 | Standard tolerance | Channel width, leg height, wall thickness, parallelism and twist | Sliding tracks, cable covers, edge channels and supports | Specify internal width when the profile must accept a panel, insert or moving component. |
| Unequal-angle profile | 40 × 20 × 3 to 120 × 60 × 10 | 3.0 to 10.0 | Special tolerance by agreement | Each leg length, included angle, corner radius and twist | Offset brackets, asymmetric frames and equipment supports | Use a drawing with clearly identified datum legs because unequal geometry increases inspection sensitivity. |
| Multi-void architectural or technical profile | 40 × 40 to 200 × 100 | 1.5 to 5.0 | Special tolerance by agreement | Overall dimensions, internal void dimensions, wall thickness, contour, twist and straightness | Door, window, façade and technical enclosure components | Identify visible surfaces and functional interfaces separately; cosmetic requirements are not a substitute for dimensional tolerances. |
| Precision mounting profile | 20 × 20 to 80 × 80 | 2.0 to 5.0 | Special tolerance by agreement | Datum width, slot position, slot opening, parallelism, straightness and twist | Linear motion assemblies, sensor mounts and modular machine structures | Apply special requirements only to functional datums and verify the effect of profile length on straightness and twist. |
| Heat-sink or finned profile | 30 × 20 to 180 × 100 | Base wall 2.0 to 8.0 | Special tolerance by agreement | Base flatness, fin height, fin spacing, fin thickness and overall width | Power electronics, LED systems and industrial cooling assemblies | Control the base surface separately when thermal contact resistance is critical; fin dimensions may require process-specific agreement. |
How to Choose Industrial Aluminum Profiles in 2026?
When selecting industrial aluminum profiles, specify the anodizing class under EN ISO 7599. The class indicates the nominal coating thickness in micrometres. AA10 provides 10 μm, AA15 provides 15 μm, AA20 provides 20 μm, and AA25 provides 25 μm.
Choose the class according to exposure, handling, and expected service life. AA10 may suit protected indoor components with limited abrasion. AA15 offers a practical option for general industrial interiors and sheltered areas. AA20 is more suitable for outdoor profiles facing moisture, sunlight, and regular cleaning. AA25 provides a thicker barrier for demanding environments, but thickness alone cannot solve poor surface preparation.
Inspect the full specification, not one number. Confirm the aluminum alloy, pretreatment, sealing quality, color tolerance, and inspection method. EN ISO 7599 should be named directly in the purchase documents. Request coating measurements from representative areas, including edges and concealed faces where practical. Small details matter.
A thicker coating is not always better. It can increase cost and may reveal surface defects more clearly. I have seen specifications choose AA25 without checking the actual environment. That approach needs reconsideration. Salt exposure, trapped water, and harsh cleaners can still shorten service life. Ask the processor to confirm the selected class and provide test records before production approval.
A reliable selection starts with documented ASTM B221 compliance. Request the alloy, temper, dimensions, and applicable tolerance records. Do not accept a generic certificate without checking heat numbers and traceability. ASTM B221 supports extrusion requirements, but it does not define every finished-part expectation. Specify surface finish, straightness, hole positions, and cutting tolerances separately. Small gaps here can create expensive assembly problems later.
Inspect fabrication quality with practical evidence. Cut ends should be square, clean, and free from heavy burrs. Check drilled holes with actual fasteners, not only drawings. Examine anodized or coated surfaces under consistent lighting. Color variation may indicate process inconsistency, although appearance alone cannot prove performance. Ask for inspection samples and dimensional reports. Photos help, but physical samples reveal more. I have seen polished samples hide weak packaging and careless handling. That mistake is easy to repeat.
Lifecycle cost deserves equal attention. Compare material price, machining time, scrap, maintenance, and replacement access. A slightly higher-grade profile may reduce deflection and installation labor. Calculate the cost of downtime, not only the invoice total. Consider corrosion exposure, cleaning needs, and future modifications. A cheap profile can become expensive after one redesign. Spreadsheets can still mislead. Recheck assumptions with production staff and installers before approval. The best choice is often the one that performs predictably, not the one with the lowest initial price.